If you’ve ever watched a tiny, intricate medical implant take shape from a solid block of titanium, or a precision aerospace bracket that has to fit within a hair’s breadth of tolerance, you’ve probably wondered what makes that machine so much better than the old clunky mills most shops have used for decades. As someone who’s been selling high precision vertical machining centers (VMCs) for years, I get this question all the time. People throw around terms like “accuracy” and “rigidity” like they’re buzzwords, but there’s a whole lot that goes into what makes a VMC “high precision” vs. just a regular run-of-the-mill model. Let’s break this down, no stuffy industry jargon, just the real deal from someone who’s stood next to these machines while they’re carving parts that can make or break a customer’s business. High Precision Vertical Machining Center

First off, let’s talk about tolerance, because that’s the whole point of a high precision VMC. Most standard VMCs will hold tolerances of around +/- 0.001 inches, right? But when you’re dealing with aerospace, medical, or even semi-conductor parts? That’s way too loose. A high precision VMC can easily hold +/- 0.0002 inches, sometimes even tighter, depending on the application. Wait, let’s put that in perspective: 0.0002 inches is about the thickness of a human hair. Yeah, that small. How do they do that? It’s not just one thing, it’s a bunch of little design choices that add up. For starters, the linear motion systems aren’t your basic ball screws you find on entry-level mills. We use high-precision ball screws that are ground to microns, not just machined, and they’re often preloaded to eliminate any play, backlash, or “slop” as we call it in the shop. No one wants their tool drifting 0.0005 inches mid-cut, that’s a scrapped part before you even finish.
Then there’s the way the axes move. High precision VMCs almost always use linear guides instead of traditional slide ways. Slide ways work with a lubricated film, which is fine for rough cutting, but linear guides use rolling elements (think tiny ball bearings or rollers) that make movement super smooth and consistent, no stick-slip effect. Stick-slip is that little jerk when the axis starts moving after being stationary, right? That’s the enemy of precision, especially for small, detailed features like micro-grooves or threaded holes that are only a few thousandths of an inch wide. We’ve had customers come to us who were fighting this on their old mills, and switching to a high precision VMC cut their scrap rate by 40% almost overnight. That’s not just a number, that’s thousands of dollars saved every month.
Next up, rigidity. This is make or break for precision, especially when you’re cutting hard materials like titanium, Inconel, or hardened steel. If the machine frame twists or bends even a tiny bit when you apply cutting force, your tolerance goes out the window. Entry-level VMCs often use cast iron frames that are lighter to keep costs down, but we use heavy-duty, stress-relieved cast iron (sometimes even natural granite for some specialty models) that doesn’t shift or vibrate, even when you’re running a ½-inch end mill at full speed into a 1-inch block of stainless steel. The spindle is another big part of rigidity. A high precision VMC spindle isn’t a cheap belt-driven unit that hums along. Most are direct-drive or gear-driven with precision bearings, often high-speed angular contact or ceramic bearings that can handle both high RPM and heavy cutting forces without flexing. We tested this once: a customer was cutting titanium brackets for fighter jets, and their old belt-driven spindle would flex enough to create a 0.0008 inch error in the side profile. Switched to a high precision VMC with a direct-drive spindle, that error dropped to 0.0001 inch. Game over for their scrap problems.
Wait, I can’t skip thermal stability. This is the part that surprises a lot of people, because it’s not obvious until you’ve dealt with it. Machines expand when they get hot, right? Whether it’s from the spindle running for hours, the coolant pump, or even the shop’s AC kicking on and off, heat causes the machine’s parts to expand, throwing off your alignment. A high precision VMC is designed to fight this. We have integrated thermal compensation systems that use temperature sensors all over the machine frame, spindle, and ball screws, and the CNC automatically adjusts the axis positions in real time to counteract any expansion. Some of our top models even have a thermally symmetric design, meaning the left and right sides of the machine heat up at the same rate, so there’s no uneven expansion that twists the frame. I had a medical device customer who was making 1,000 hip implants a week. Their old machine would drift 0.0003 inches over a 12-hour run, so they had to stop and recalibrate every 4 hours. With our thermal-stable VMC, they run a full 24-hour shift without any drift. That’s 6 extra hours of production a day, no extra work on their end.
Then there’s the CNC control. It’s not just any old controller you can buy off the shelf. High precision VMCs use advanced CNC systems that can handle super high resolution, down to nanometers, not just thousandths of an inch. They also have look-ahead functionality that reads your part program ahead of time, so it can adjust feed rates and acceleration to keep the movement smooth, no sudden jerks that cause vibration or error. Some controllers even have advanced error mapping, where you input the exact geometric errors of each axis, and the controller compensates for them automatically. This is huge for complex parts like turbine blades or mold inserts that have curved surfaces that have to be perfect. I once had a tool and die maker come to us, saying their old controller couldn’t keep up with the 5-axis machining they needed for a plastic injection mold cavity. With our high precision VMC’s CNC, they were able to cut the cycle time for each mold by 25% and the rejection rate went from 12% to less than 1%.
Oh, and let’s talk about tool holding, something that’s easy to overlook but critical for precision. If your tool holder isn’t perfectly aligned, you’re going to get runout, which means the tool is wobbling as it spins, so the cut isn’t consistent. High precision VMCs use HSK or CAT (when appropriate) tool holders that are precision-ground to tight tolerances, and they have a taper that fits the spindle with very high accuracy. Some even use hydraulic or heat-shrink tool holders instead of collets, because they eliminate any tiny gaps or movement in the tool. We’ve seen customers who were using cheap collet holders get 0.0005 inches of runout at the tool tip, and switching to precision holders dropped that to 0.0001 inches. That difference translates directly to a better part.
Another feature that’s common but often misunderstood is axis resolution. Entry-level VMCs might have a encoder that counts every 0.0001 inches, but high precision models count every 0.00001 inches, sometimes even smaller. That means every tiny movement the machine makes is exactly where it’s supposed to be, no guessing, no slippage. When you’re cutting a part with hundreds of small features, that resolution adds up to a perfect finish. No more rough edges, no more misshapen holes.
Wait, let’s not forget about vibration damping. Even if your frame is rigid, vibration from cutting can throw off your precision, especially for thin-walled parts or delicate features. High precision VMCs have designs that dampen vibration, like ribbing in the cast frame, or even active vibration cancellation in some high-end models. I had a customer who was making small electronic connectors with thin walls that would vibrate and get deformed on their old machine. Our high precision VMC’s vibration damping let them run at full speed without any deformation, so they didn’t have to slow down their feed rate and waste time.
Now, before you think this is all just tech talk, let’s get real about what this means for you. Buying a high precision VMC isn’t just about having a fancy machine in your shop. It’s about scrap parts that don’t have to be thrown away, production times that don’t require constant recalibration, and being able to take on jobs that your competitors can’t. I’ve seen shops go from turning down aerospace contracts because their parts couldn’t hold the tolerance, to winning every bid once they got our high precision VMCs. I’ve seen medical device makers cut their production costs by 30% because they no longer have to rework parts.
But here’s the thing: not every “high precision” VMC is the same. A lot of manufacturers slap a new label on an entry-level model and call it high precision. That’s why you have to look for the features we talked about: preloaded ball screws, linear guides, stress-relieved frame, thermal compensation, high-resolution CNC, precision tool holders. These aren’t extra add-ons, they’re core to what makes the machine actually deliver the precision you need.
If you’re someone who’s tired of scrapping parts, missing tolerance requirements, or turning down big jobs because your machine can’t keep up, let’s have a chat. I’ve been in this game long enough to know exactly what works for different industries, whether you’re a small tool shop making custom molds, a mid-sized aerospace supplier, or a medical device manufacturer. We don’t just sell machines, we help you figure out exactly what your needs are, and what model will fit your shop and your budget. We’ve installed these machines in shops all over, and every time, the feedback is the same: this isn’t just a better mill, it’s a game-changer.
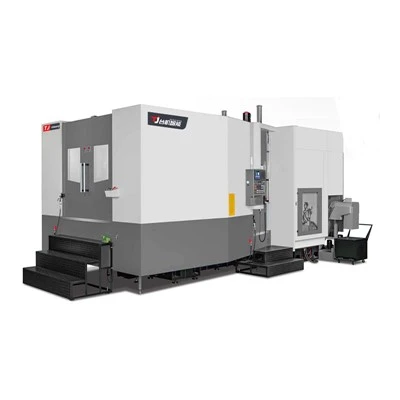
At the end of the day, a high precision vertical machining center isn’t about numbers on a spec sheet. It’s about being able to produce parts that are perfect, every single time, even when you’re running 24/7, even when you’re cutting the hardest materials. If that’s what you need for your business, let’s connect and talk through what you’re working on.
Five Axis Machining Center References
- Boothroyd, G., & Knight, W. A. (2006). Fundamentals of Machining and Machine Tools. CRC Press.
- ISO 10360-2:2009, Geometrical Product Specifications (GPS) – Acceptance and reverification tests for coordinate measuring machines (CMM) – Part 2: CMMs used for measuring linear dimensions.
- Shin, Y. C., & Waters, A. (2018). Thermal error compensation in machine tools: A review and some perspectives. International Journal of Machine Tools and Manufacture, 134, 1-18.
- Weck, M., & Brecher, C. (2005). Machine Tools: Structure and Control. Wiley-VCH.
- Zuperl, U., & Cus, F. (2007). Effect of tool runout on the milling process. Journal of Materials Processing Technology, 186(1-3), 197-203.
Guangdong Taiji Intelligent Equipment Co., Ltd.
Address: Room 107, Building 15, No. 911 Jian’an Road, Chang’an Town, Dongguan City, Guangdong Province
E-mail: sale@gdtaijicnc.com
WebSite: https://www.gdtaijicnc.com/
